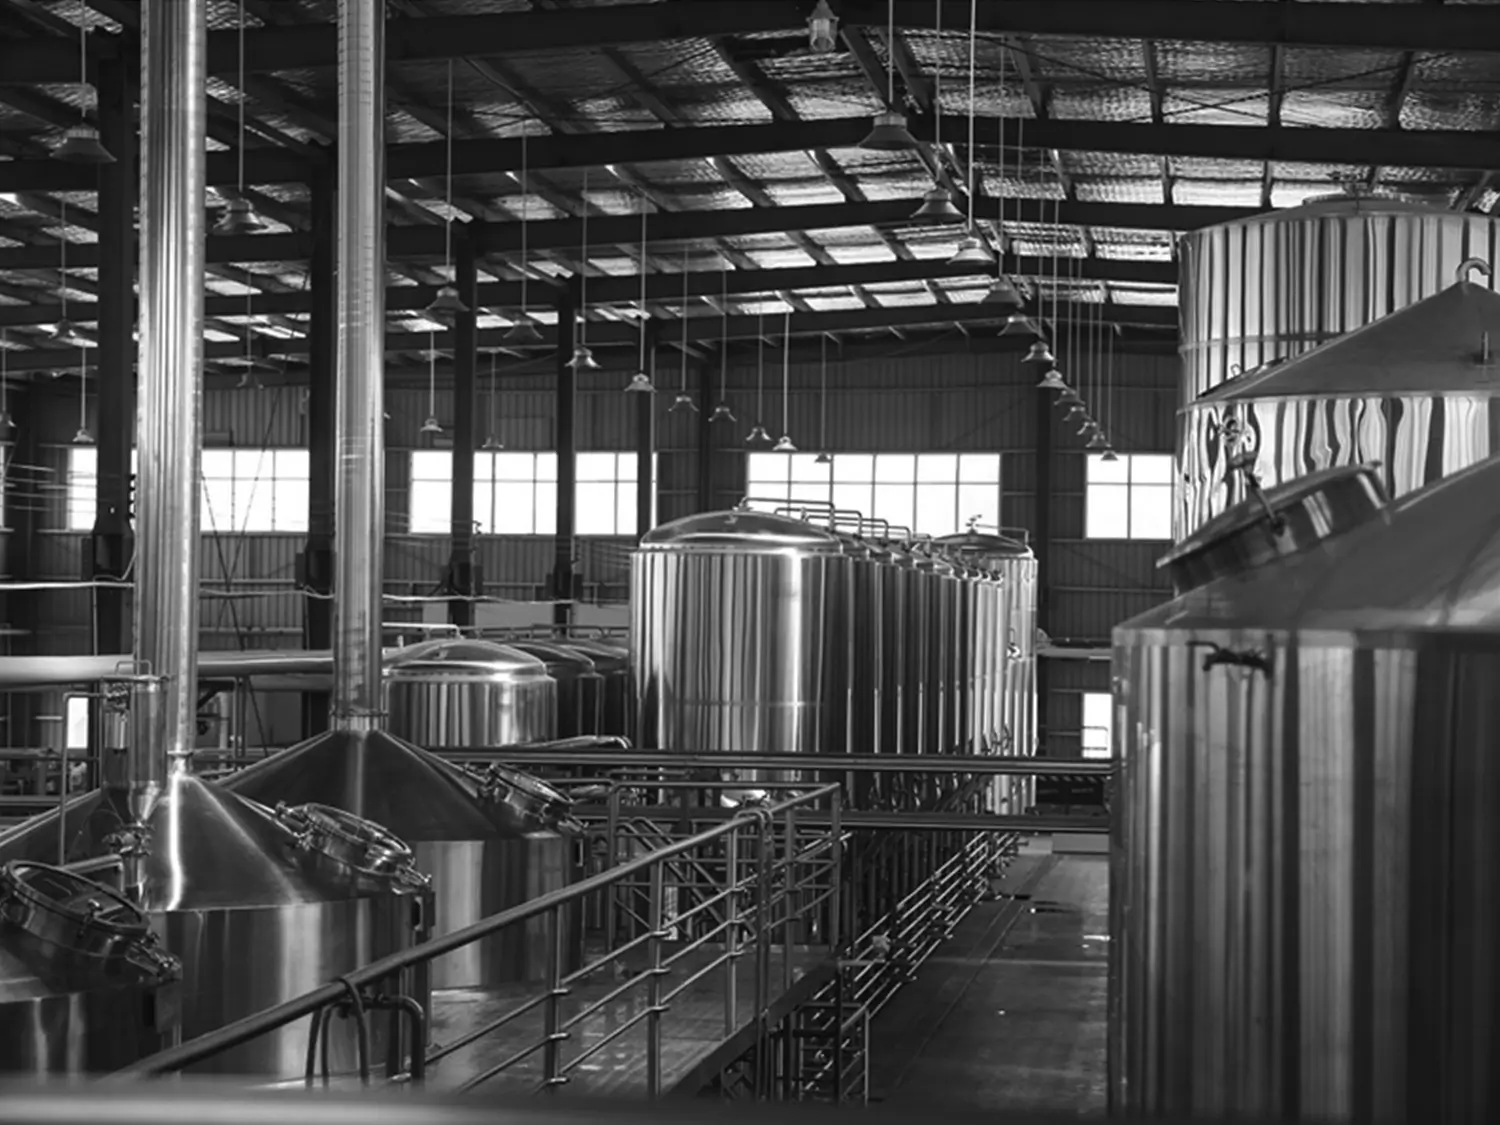
5000L Commercial Brewery Equipment (50HL)
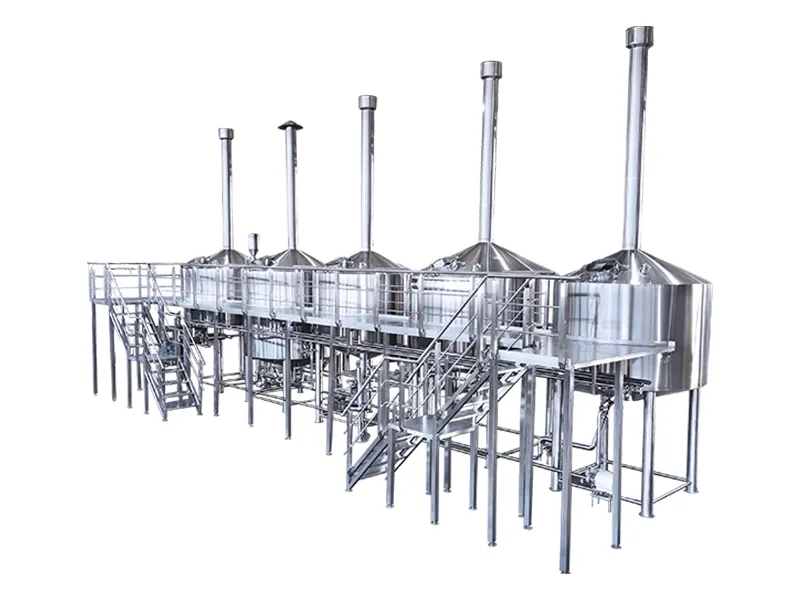
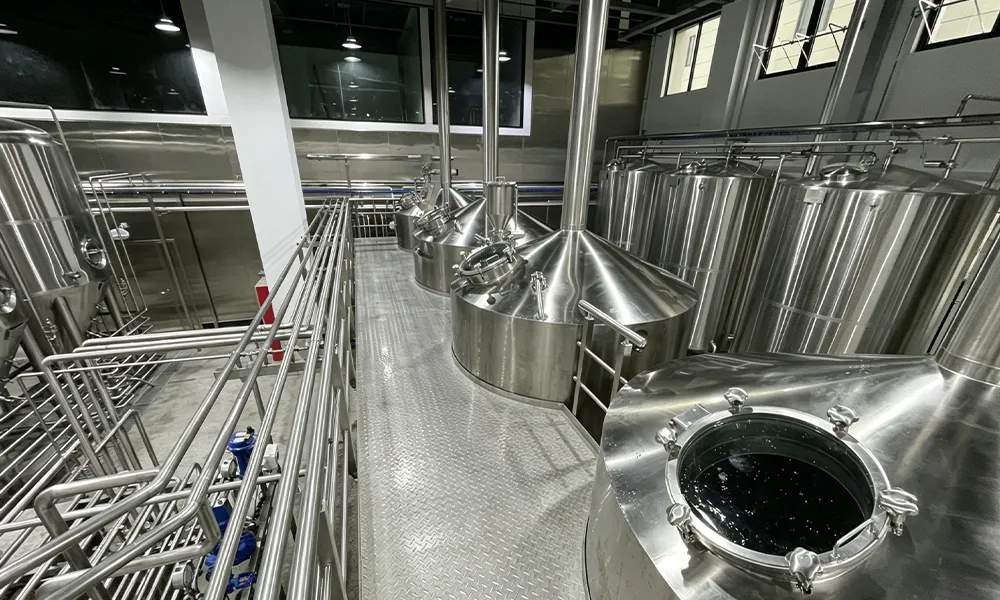
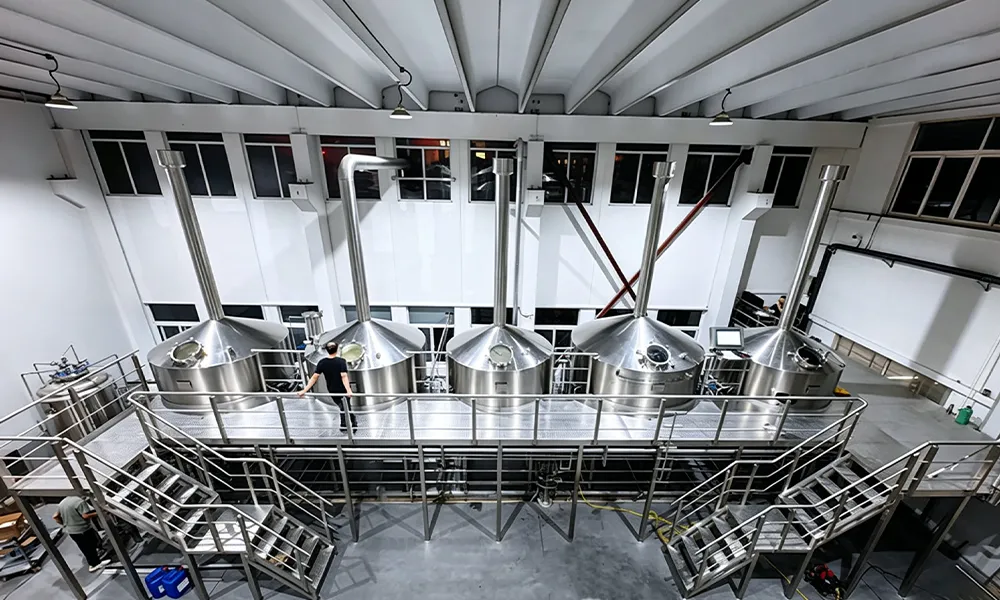
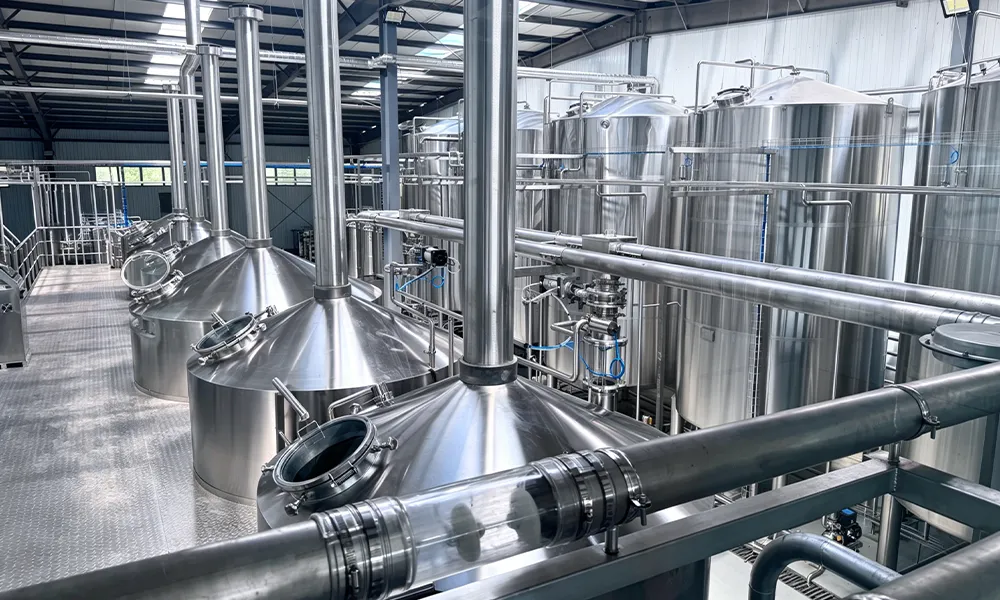
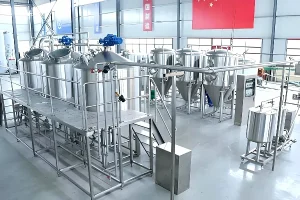
5000L commercial brewery equipment for high-volume craft and contract production, with five-vessel brewhouse, large cellar, CIP, cooling and automation from METO.
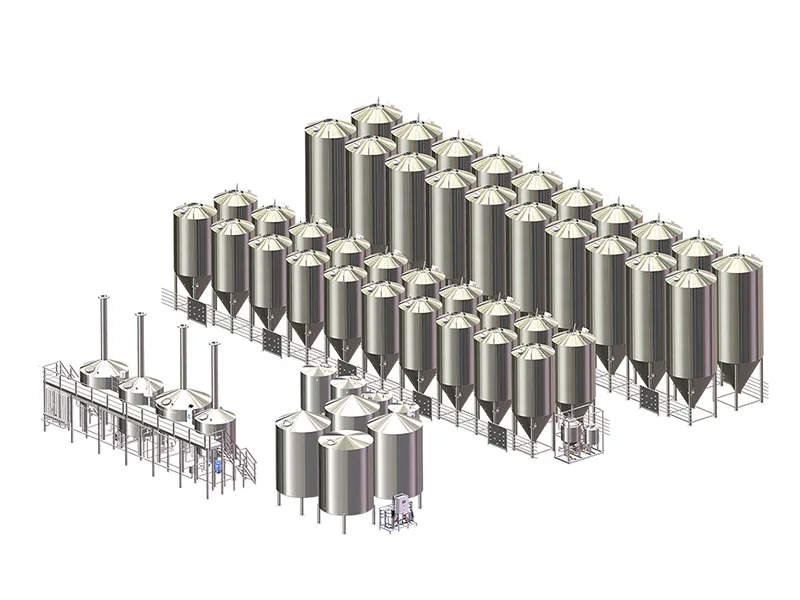
5000L commercial brewery equipment for high-volume craft and contract production, with five-vessel brewhouse, large cellar, CIP, cooling and automation from METO.
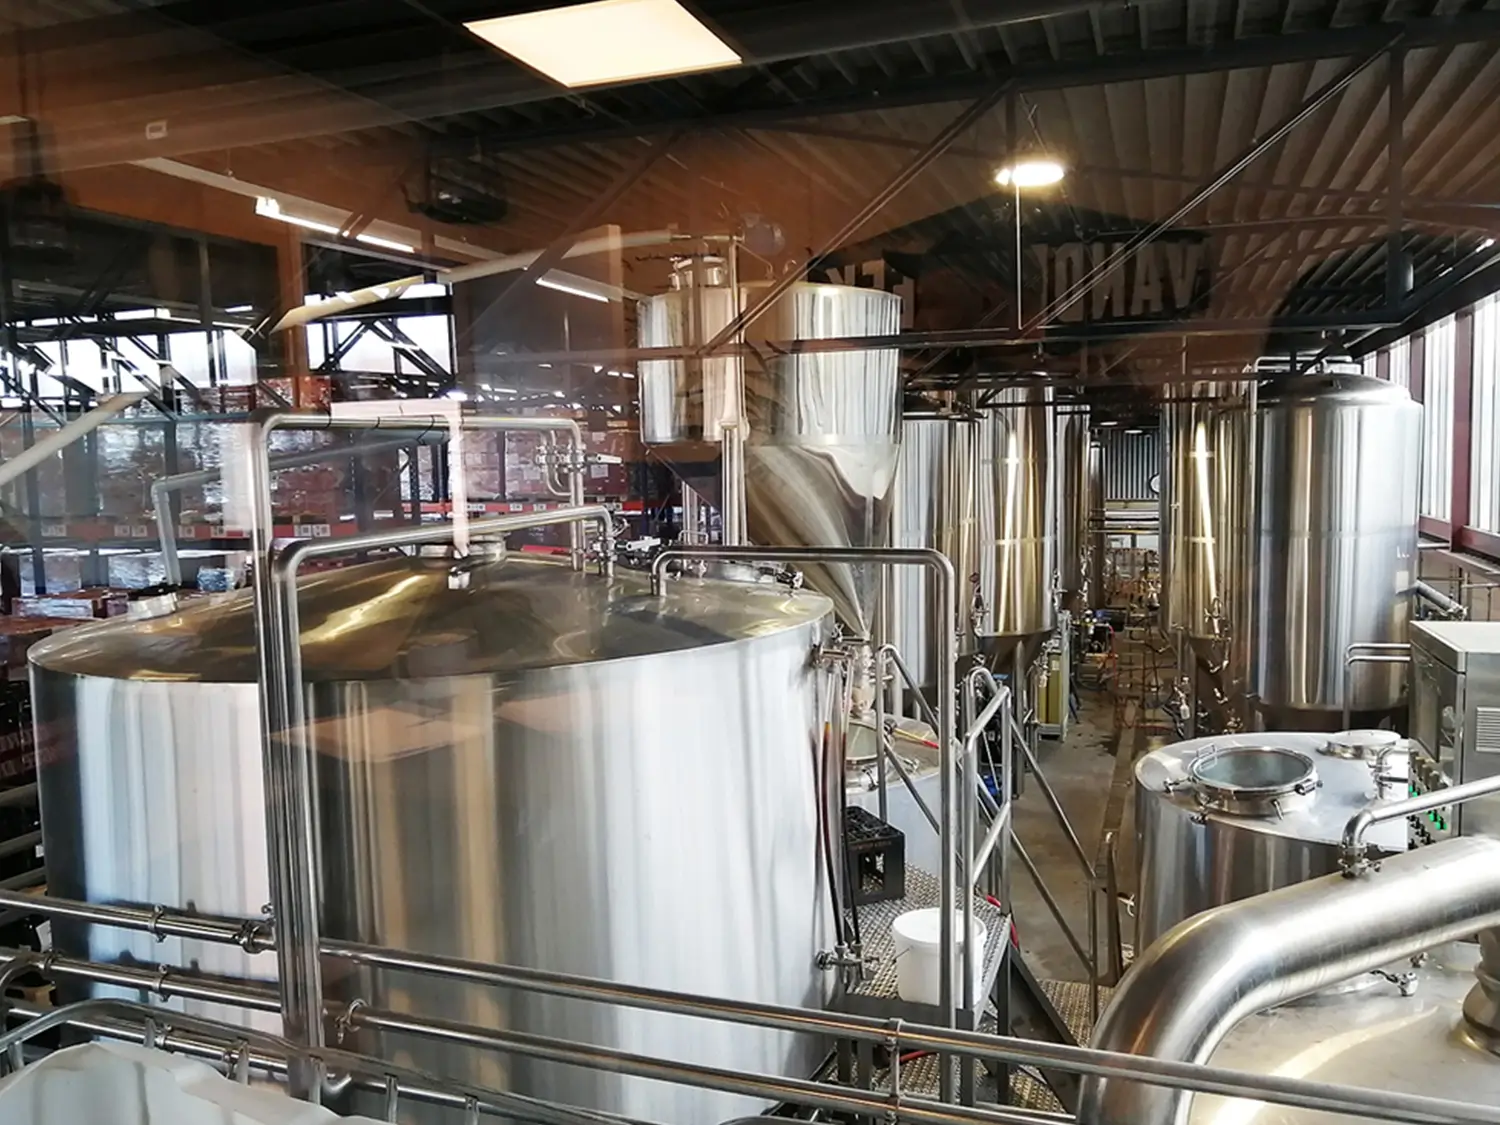
3500L commercial brewery equipment for regional and contract brewing, with five-vessel brewhouse, scalable cellar, cooling, CIP and automation from METO.
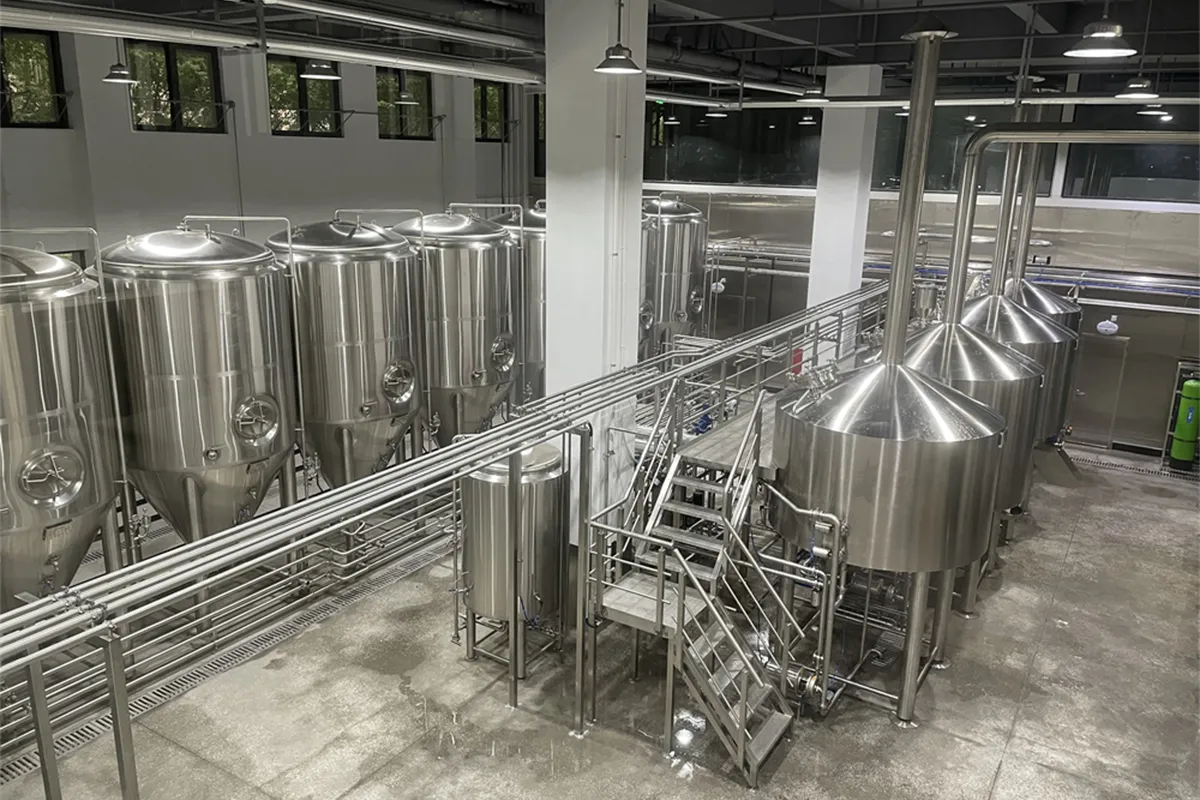
2500L commercial brewery equipment with a five-vessel brewhouse, fermentation cellar, glycol cooling, CIP, automation and optional packaging integration from METO.
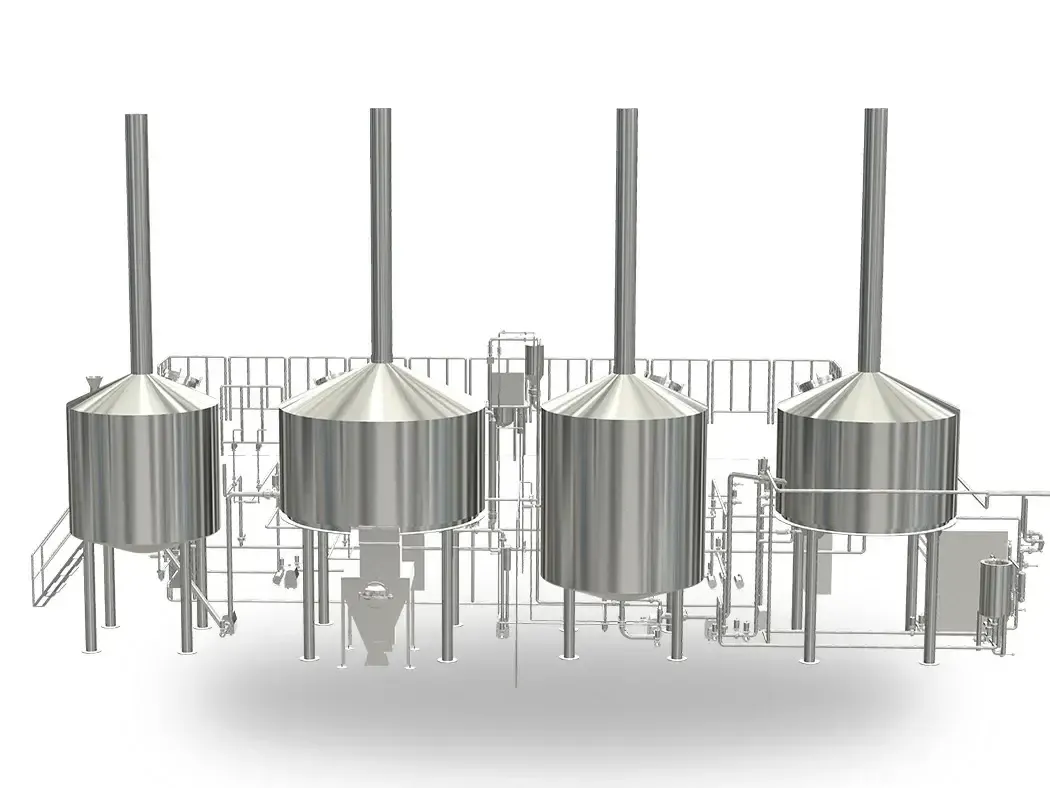
2000L commercial brewery equipment with multi-vessel brewhouse, fermentation cellar, glycol cooling, CIP, automation and optional packaging integration from METO.

Location: USA
Website:https://sturgeonspirits.com/
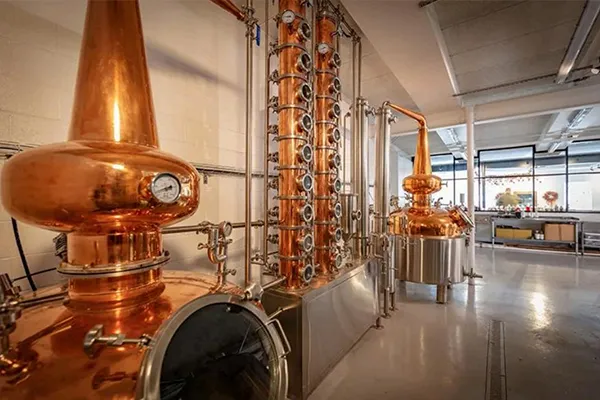
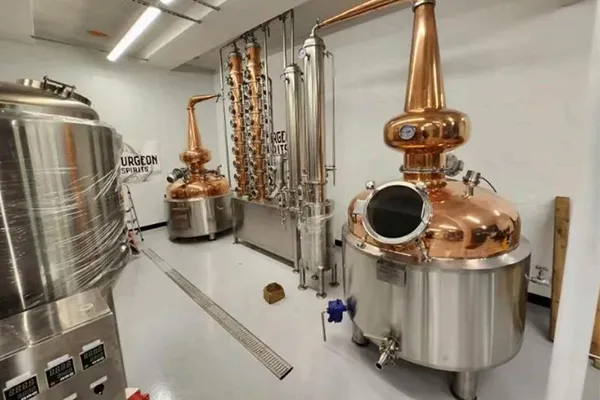
In 2021, to expand production capacity and improve product quality consistency, Sturgeon Spirits invested in a complete 500L distillation system from Meto, a professional manufacturer of distillation equipment. The system covers the entire production process, from milling and mashing to fermentation and distillation. In addition to supporting traditional distillation methods, the equipment offers a high level of flexibility, making it suitable for producing a wide range of spirits such as vodka and gin. This investment has become a key technical driver supporting the continued growth of Sturgeon
Spirits.
In the early stage of equipment selection, the Sturgeon Spirits team conducted extensive research on distillation equipment suppliers that could meet U.S. safety standards, offer flexible system customization, and support craft spirits production such as vodka and gin.
After comparing multiple manufacturers, Meto stood out due to:
• Proven experience in micro distillery projects
• Ability to provide UL-certified motors and electrical components
• Strong customization capability for column stills and gin systems
• Clear technical communication and fast engineering feedback
Through direct communication with Meto’s engineering team, Sturgeon Spirits shared their production goals, spirit styles, and space requirements.Meto then proposed a fully customized 500L distillation solution, covering the complete process from milling to fermentation and distillation, which matched their expectations perfectly.
The following are the parameters of the Distillery Equipment for whisky/rum/gin:
• Milling System 150Kg/h
• 500L Mash Lauter Tank
• 1000L Hot Water tank, Electric Heating+3T hot water pump
• 500L*3 Fermentation Tank/Unitank (Double Layer)
• 5 HP Chiller
• Mobile CIP Pump
• Control System-PID Digital Type
• 500L No Jacketed Mixing Tank
• 500L Distillation Equipment with Control Cabinet–With Gin Basket
• 500L Still
• All Motors with UL Certificated
• All Electronics ofControl Cabinets WithUL Certificated
• Two 500L Stills With both Electric Coils and Steam Jacket
1 Complete One-Stop Distillery Solution
Meto provided a full turnkey system, including milling, mashing, fermentation,chilling, CIP cleaning, distillation, and control systems. This integrated approach simplified project coordination and ensured compatibility across all
equipment.
2 Flexible Customization for Craft Spirits
The system was tailored to support multiple spirit types, especially gin production:
• Integrated gin basket
• Upgraded 8-inch diameter column
• Expanded from 6 plates to a total of 18 plates, enabling higher purity,
better separation, and more precise flavor control
This flexibility allows Sturgeon Spirits to easily adjust recipes and experiment with new products.
3 Compliance with U.S. Standards
All motors and control cabinet electronics were supplied with UL certification,ensuring compliance with U.S. electrical safety requirements and facilitating smooth installation and inspection.
4 Dual Heating Options for Maximum Versatility
The two 500 L stills were designed with both electric heating coils and steam jackets, allowing operators to choose the most suitable heating method based on production needs, energy availability, and operating costs.
5 Professional Engineering Support & Fast Response
Meto’s engineering team provided:
• Clear technical drawings and configuration confirmation
• Detailed control logic via PID digital control systems
• Efficient communication throughout production and delivery
This professional support significantly reduced project risk and installation time.
By choosing Meto, Sturgeon Spirits successfully built a reliable, scalable, and future-ready distillery system. The equipment not only supports current production but also leaves room for future expansion and product diversification.
This project reflects Meto’s core philosophy:
engineering-driven design, compliance-focused manufacturing, and long-term value for craft distilleries worldwide.
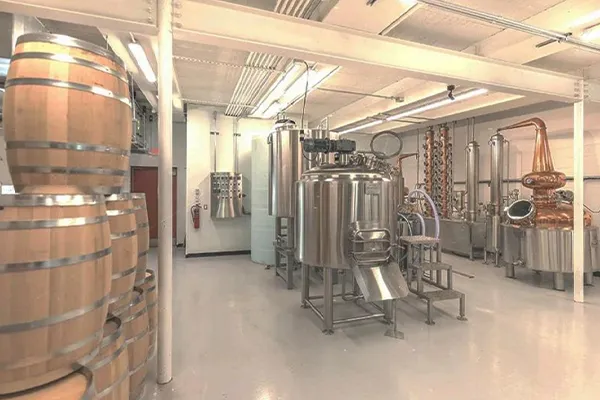
Sturgeon Spirits is a craft distillery located in Oshkosh, Wisconsin, USA. The distillery is dedicated to producing high-quality craft spirits, including vodka, gin, rum, and other styles, while creating a distinctive brand experience and
strong community culture. With a focus on small-batch, on-site distillation,handcrafted blending, and local character, Sturgeon Spirits offers an engaging visitor experience and has become a must-visit craft distillery in the region.
Location: Chile
Website:https://destileriapetricor.com/
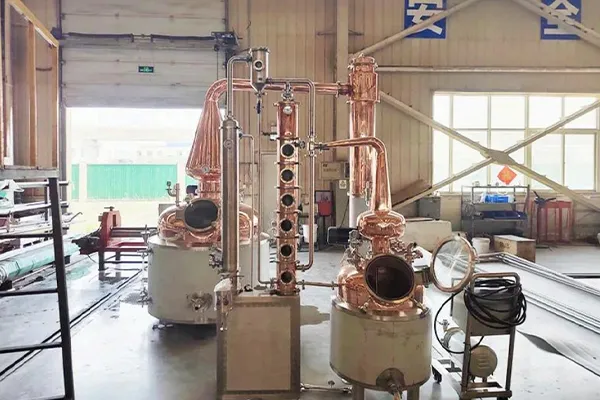
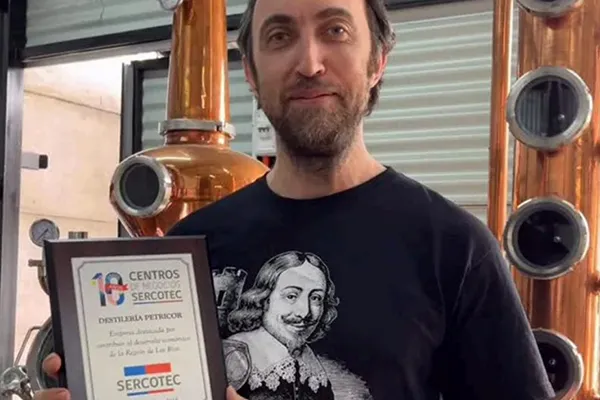
In 2025, Petricor Destilería, a renowned craft distillery from Chile, decided to upgrade its production equipment to expand its premium spirits portfolio and enhance brewing precision. After a rigorous screening and comprehensive evaluation of global manufacturers, Petricor Destilería selected Meto via Aliba ba.com and proceeded to purchase a high-performance 500L double-layer insulated distillation system.
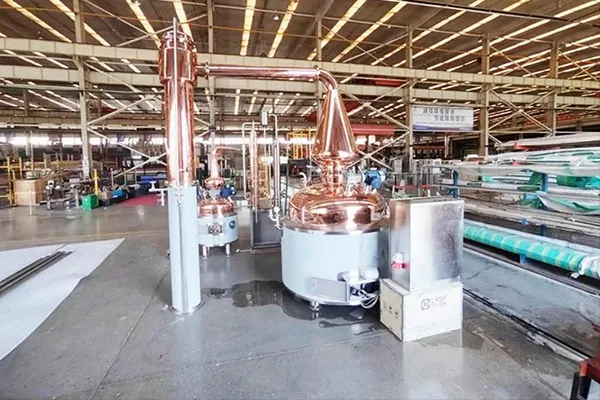
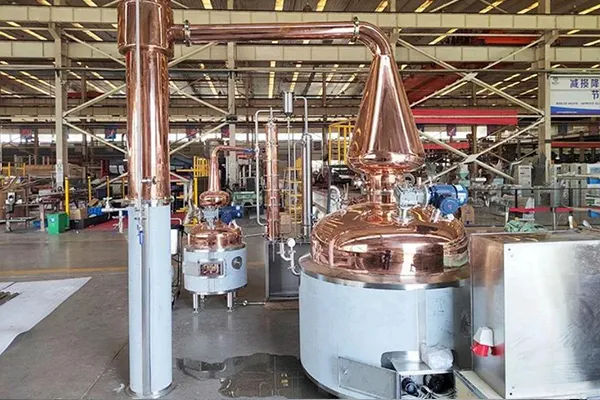
To meet the client’s high standards for distillation efficiency and spirit purity,Meto customized a complete distillation solution. With a core capacity of 500L,the system features comprehensive optimizations in process details:
• High-Efficiency Insulated Still: The core still features an advanced double-layer tank design with professional insulation. This significantly reduces heat loss, ensuring consistent temperatures during distillation and
maximizing energy efficiency.
• Precise Fraction Extraction: Equipped with a classic Swan neck and Lyne arm combination. This design effectively increases the reflux ratio, helping the distillery accurately remove impurities from the heads and tails to
extract a purer, better-flavored heart cut.
• Powerful Condensing System: Features a high-efficiency condenser to ensure alcohol vapors are rapidly and fully liquefied, guaranteeing both yield and spirit stability.
• Intelligent Control & CIP: The integrated system includes an advanced automation control module, allowing distillers to monitor and adjust parameters in real-time. Additionally, it is equipped with a professional CIP (Cleaning-in-Place) pump for automated cleaning, greatly reducing manual maintenance costs and improving hygiene standards.
Through seamless communication on Alibaba.com, the Meto team maintained close contact with Petricor Destilería. From solution design and manufacturing to final cross-border delivery, Meto provided professional technical support
throughout the entire process. The successful delivery and commissioning of this 500L distillation equipment not only helped Petricor Destilería achieve a dual leap in capacity and quality but also reaffirmed Meto’s exceptional strength and global service capabilities in the craft distillation equipment industry.
If you are also interested in our brewery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location:Vienna, Ontario, Canada
Website: https://ottercreekdistilling.ca/
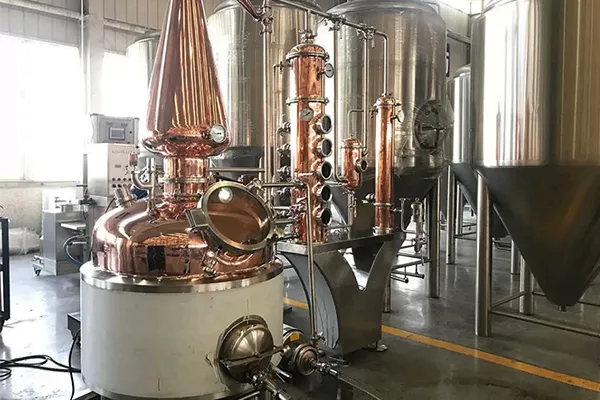
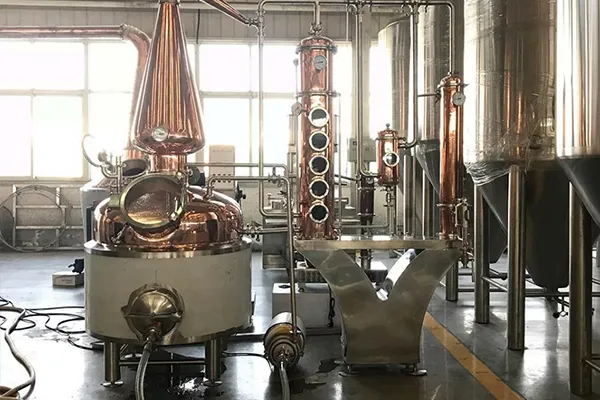
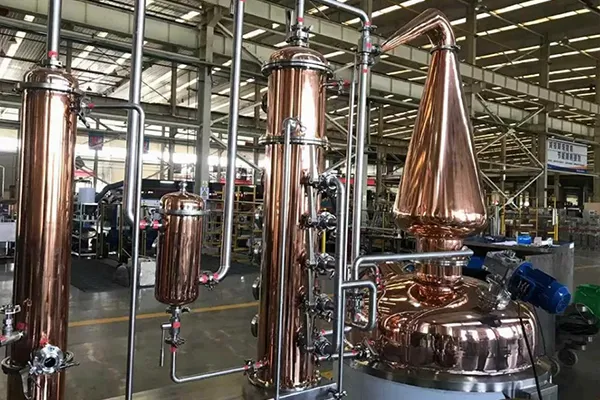
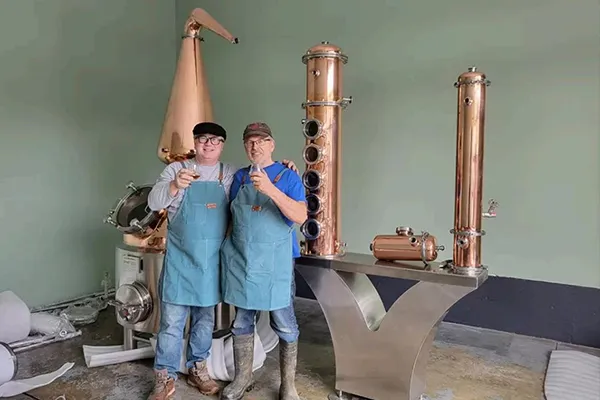
In June 2023, we received an inquiry for a distiller from a client in Ontario,Canada. This client already had a small still distilling rum, whiskey, and corn liquor. The product had an alcohol content of 65% and they wanted to expand
production. After a month of discussion, they finalized the following
configuration:
1.300L copper still pot, electric heating with a dry-boil level gauge.
2.Copper column with 4 plates and a copper dephlegmator.
3.Copper gin basket
4.Copper condenser.
5.Agitator with CSA-certified explosion-proof motor.
6.Explosion-proof CSA-certified pumps for transfer mashing and CIP.
7.All electrical components in the control cabinet are CSA-certified.
When the customer received the 300L distiller, he was very excited and shared the on-site pictures with us. He also gave us a 5-star review: “It looks like pretty high equipment. The price was excellent and the sales (Fairy) was excellent and responded quickly to questions.”
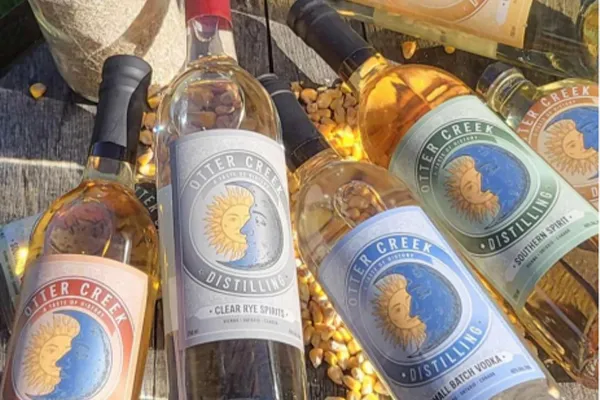
It’s no secret that Ontario whiskey has long held a significant share of the US market and accounts for 75% of Canada’s total production. Ontario whiskey is primarily made from continuously distilled grain whiskey (primarily corn), blended with pot still rye whiskey for added depth, creating the signature “world’s lightest whiskey” with a smooth, easy-drinking flavor.While rye is a key ingredient in the production of various grains, including corn and barley malt, it’s rye that is key to its flavor. Using rye as a key ingredient, several classic spirits have been launched: Clear Rye Spirit, Gold Star Gin, Southern Spirit, and Small Batch Vodka.
If you are also interested in our distillery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable distillery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location:Australia
Website: https://www.innesdistillery.com.au
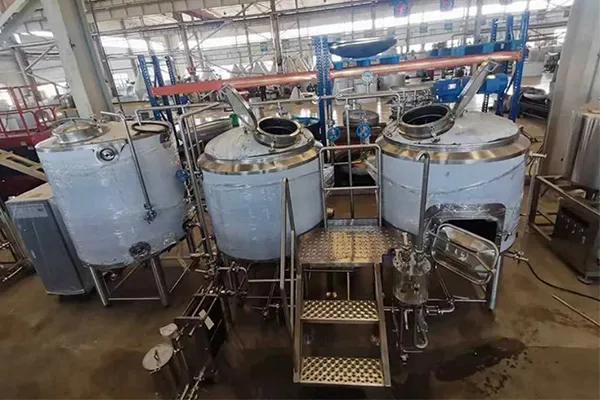
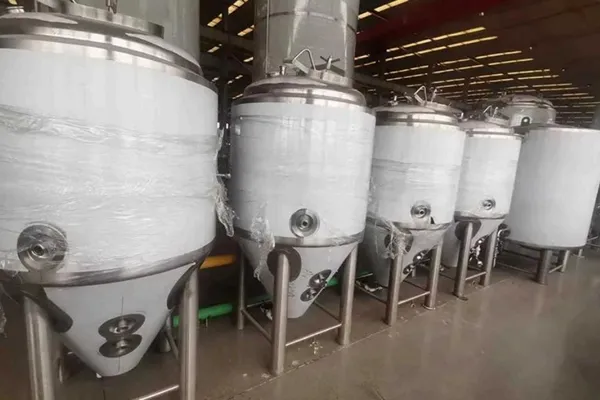
The Australian client purchased a complete 500L brewery system together with professional distillation equipment from our company. The 500L brewhouse is ideal for craft breweries, brewpubs, and taprooms that require both stable
output and flexibility for recipe development.The brewhouse is equipped with a 2-vessel brewhouse using steam heating,
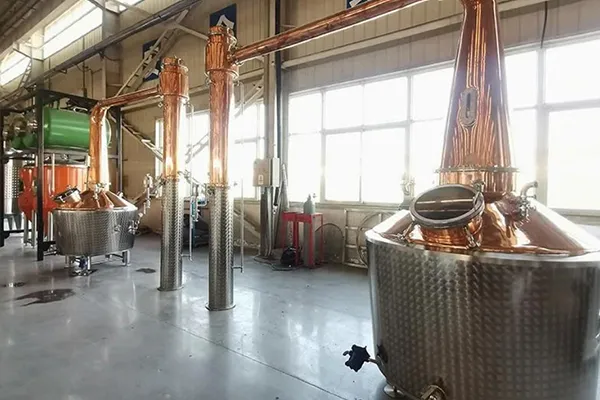
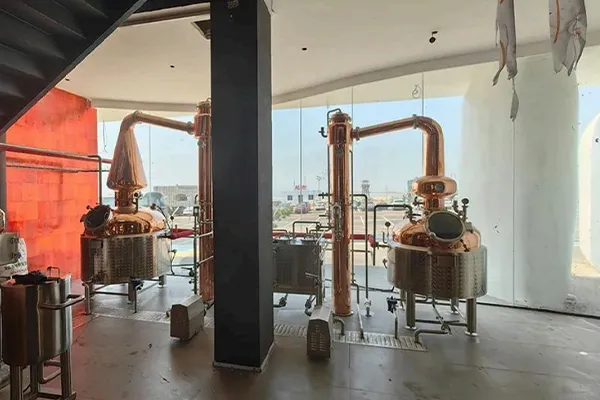
SUS304 pipelines, glycol cooling, a CIP unit, and PLC automation. This ensures stable performance, precise process control, and efficient daily operations. The distillation system is engineered with a copper pot still, rectification
column, dephlegmator, condenser, and collection tanks. Copper components enhance spirit purity by removing sulfur compounds, while the column design allows better separation and control of aromatic fractions. Together, these
features enable the production of premium-quality whiskey, gin, and rum with repeatable results.This not only broadens their product portfolio but also supports on-site experiences and brand growth by offering both freshly brewed beer and
handcrafted spirits within the same venue.
• Milling System 100-150 Kg/h
• 500L 2 Vessels Brewhouse(MT/LT+KWT) + 800L Hot Water tank, Steam
Heating
• SUS304 5m2 heat exchange
• 500L*4 Fermentation Tanks/Unitanks
• 1500L Glycol water tank +5HP Chiller
• PLC Control System
• CIP System
• 500L-1000L Pot still
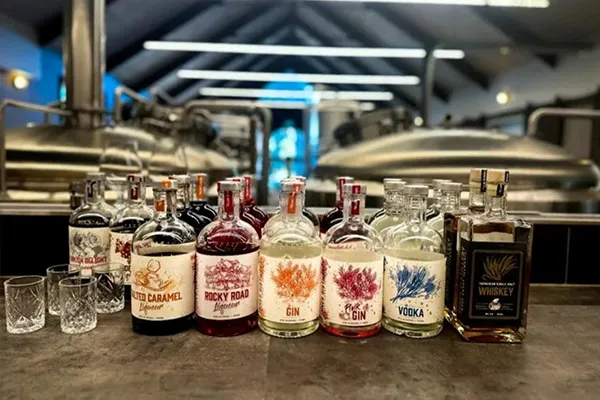
Innes Distillery, pioneers on the West Coast of Tasmania, is located in the lakeside town of Tullah, surrounded by pristine mountains, pure rainwater, and clean air. Inspired by the story of two brothers who discovered mineral riches
in the wilderness, the distillery reflects a spirit of exploration and craftsmanship. Specializing in handcrafted gin, vodka, and whisky, Innes Distillery captures the natural essence of Tasmania in every batch. While its cellar door is still under construction, visitors can already enjoy selected spirits at Tullah Lakeside Lodge. With its unique location and dedication to quality, Innes Distillery is shaping a new destination for both spirit lovers and travelers in the
region.
If you are also interested in our distillery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location: Canada
Website: https://www.peaceriverbrewing.ca/
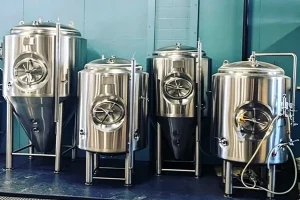
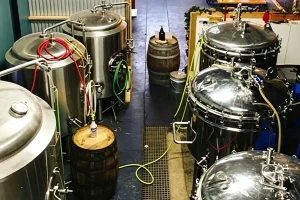
In 2020,our long-term customer from Canada, Peace River Brewing, continued to purchase from Meto, ordering 5BBL and 10BBL sake tanks and a 600L distillation system.Peace River Brewing placed an order with our company for the following equipment: – 5 BBL sake fermentation tanks – 10 BBL sake fermentation tanks – 600 L tower-type distillation equipment, comprising: distillation kettle (still), column (tower), condenser, and gin-blue (presumably a reflux or spirit-collection component)
This equipment was intended to expand their production capabilities from just beer toward distilled spirits — enabling production of gin or other craft spirits.
After delivery in 2020, Peace River Brewing integrated the equipment into their existing facility. The new distillation setup was installed along with their brewing operations, allowing them to run both beer brewing and spirit distillation under the same roof. The small footprint and moderate capacity (600 L) fitted well with their existing microbrewery/taproom layout.
The sake-tank-style fermenters (5 BBL and 10 BBL) were repurposed or used directly for fermenting mash or wash intended for distillation providing flexibility for different recipes and batch sizes.
This case demonstrates how a small craft brewery can successfully expand into craft spirits production by adopting appropriately scaled equipment — without overinvesting in oversized industrial infrastructure. By supplying 5 BBL / 10 BBL fermentation tanks and a 600 L tower-type distillation system, our company enabled Peace River Brewing to diversify, experiment, and grow, while preserving the artisanal character central to their identity.
For potential clients looking to follow a similar path, this case shows that even modest investments in the right equipment can open new product lines, improve flexibility, and broaden market opportunities, especially for small- to mid-sized craft producers.
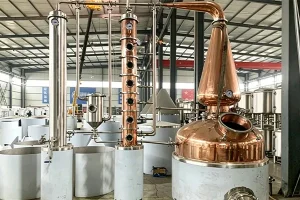
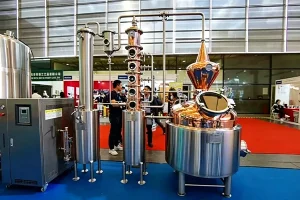
Peace River Brewing is a craft brewery and distillery located in Peace River, Alberta, Canada. Founded as a small-town microbrewery and distillery, Peace River Brewing supports handcrafted beers and spirits and hosts a local taproom offering a cozy, community-oriented atmosphere. The brewery is known for brewing small-batch beers and also producing handcrafted spirits — making it a suitable candidate for specialty equipment beyond ordinary brewing tanks.
If you are also interested in our brewery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location: Colombia
Website: https://www.hannahops.com/
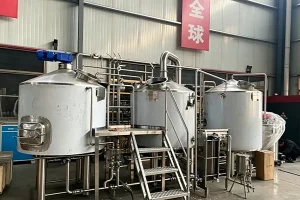
A client purchased our 1000L 2-Vessel Brewhouse System to upgrade their brewing operations. The brewhouse is fitted with pH detection and flowmeters, allowing accurate monitoring of key parameters and ensuring stable wort quality. For precise process control, two independent digital control cabinets are provided—one for the brewhouse and another for fermentation and cooling—offering reliable management across all stages of production. To expand packaging options, the project also includes a multifunctional filling machine capable of handling both cans and glass bottles. This complete setup enables the client to achieve consistent, high-quality beer production while improving efficiency and scalability. By combining advanced monitoring with flexible packaging solutions, the brewery is now better positioned to meet market demands and support future business growth.
Hanna Hops Beer Co. is a modern craft brewery based in Bogotá, Colombia, dedicated to brewing flavorful, high-quality beers inspired by creativity, passion, and community. Founded by a homebrewing enthusiast whose curiosity evolved into a full craft beer venture, the brewery focuses on using quality ingredients and refined techniques to craft distinctive styles—from easy-drinking blondes to bold, hop-forward ales. Guided by its philosophy of “Be the Brewer,” Hanna Hops celebrates individuality and the stories behind each beer, offering a welcoming space where people can share moments, explore new flavors, and enjoy the spirit of craft brewing.
If you are also interested in our brewery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location: The Netherlands
Website: https://www.muifelBrouwerij.nl
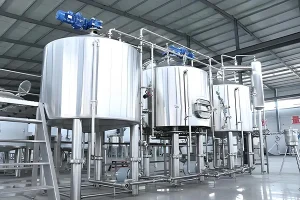
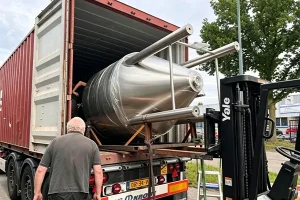
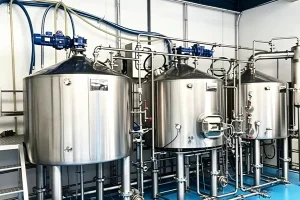
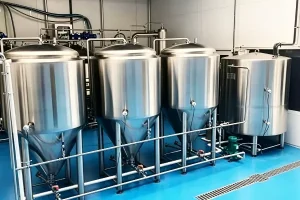
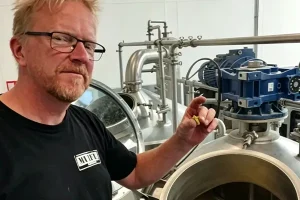
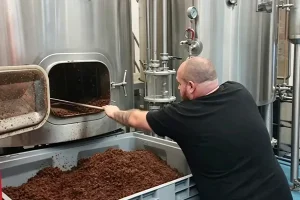
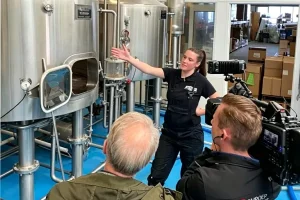
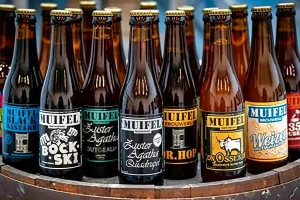
In 2018, we forged our first partnership with Muifel Brewery, supplying them with a turnkey 1000L brewing system for their new facility. From initial design consultations to final installation and commissioning, our team worked closely with their brewers, ensuring seamless communication and execution. The brewery expressed high satisfaction with both our equipment’s performance and the quality of our technical support throughout the project.
The following are the main configurations for purchasing brewery equipment:
Muifel reinforce our mission by working with a passionate team of fans. Each of us has grown from a hobbyist to a professional.
Founder Martin Ostendorf has a chemical background. combined with his many years of experience as a brewer, ensures that our beers are produced in a well-controlled craft process.
within the organization of production even after consumption, attention is paid to a virtuous and sustainable character. We also create learning opportunities for young people by providing internships.
If you are also interested in our brewery equipment, please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location: Kunming
In 2020, several expatriate founders established “Chaba” Craft Beer Bistro in Kunming. The brand name “Chaba” originates from the richly colloquial Yunnan dialect, meaning “to chat, to chime in, to banter.” The founders envisioned a place where guests could let their guard down, speak freely in a pleasant tipsy haze, and fill every gathering with laughter and joy. As a bistro that bridges Chinese and Western cultures, Chaba not only serves authentic Dai-style cuisine but is also dedicated to seamlessly blending Belgium’s sophisticated brewing techniques with the local terroir and customs of Yunnan. In terms of raw ingredients, the brewery primarily uses imported barley malt, wheat malt, hops, and yeast strains. Yet to infuse a distinctive Yunnan identity, Chaba boldly incorporates local specialty adjuncts — seasonal fruits, spices, and chili peppers — allowing every beer to brim with the spirit of the native land. Throughout the brewing process, quality and flavor consistency remain paramount. For every single batch, over 50 data points are collected, ensuring each glass of beer meets the highest standards through precise control.
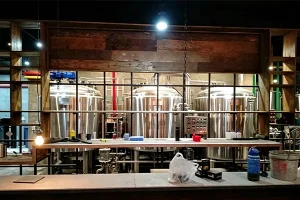
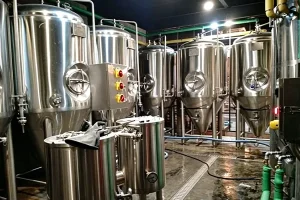
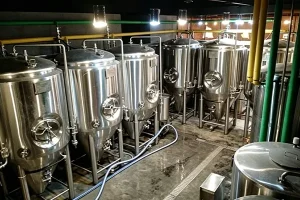
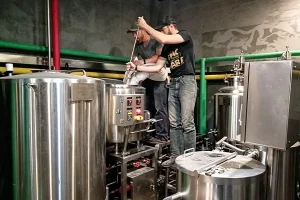
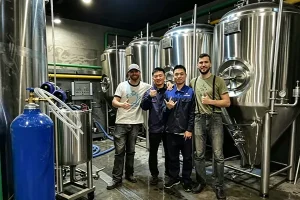
Unlike traditional bars, Chaba’s greatest highlight lies in its transparent, “brewery-in-the-front, bar-in-the-back” experience. Through the enormous clear glass window behind the stage, the entire brewhouse is laid bare before your eyes. Seven gleaming 1,000-liter fermentation tanks stand in majestic array, their formidable capacity more than enough to keep hundreds of patrons happily drinking for days. This bold architectural design completely demystifies the art of craft brewing — allowing those who love beer not just to drink well, but to truly understand the art behind the brew.
At Chaba, brewing is a rigorous scientific practice. Every morning, the brewer steps punctually into the brewhouse, picking up hydrometers and glass test tubes at the workbench, meticulously recording the parameter changes in every fermentation tank. From the moment boiling wort surges into the fermenter, to the arrival of the true “soul brewer” — the yeast — every drop of beer must undergo a fermentation and maturation process lasting as short as 20 days and as long as 60 days, before finally emerging at the bar in its freshest, most delectable form. [Core Equipment Configuration] To support high-quality craft beer production, Chaba is equipped with a professionally complete brewing and fermentation system, detailed as follows:
The craft beer game is, at its core, a conversation about the hard power of equipment and process. Chaba understands this deeply — with its 1000L American-style 3-vessel brewhouse system and seven 1,000-liter conical fermentation tanks, the brewery establishes a formidable production foundation that not only reliably supports large-scale daily supply but also provides industrial-grade assurance for the precise replication of flavor profiles. Meanwhile, the parallel 100L small-scale brewhouse system and experimental-grade fermentation tanks carve out an unrestrained creative sanctuary for the brewers, where every spark of inspiration involving local fruits, spices, and chili peppers can be refined through countless small-batch iterations before being introduced to the public. From the automated control system’s precise management of the entire brewing process, to the hygiene baseline safeguarded by the CIP cleaning cart, to the efficient packaging closed loop brought by the automatic keg filling machine — this hardware matrix, arguably leading across the entire Southwest region, not only gives full confidence to the “brewery-in-the-front” transparent brewing concept but also ensures that every glass of Chaba craft beer can withstand even the most discerning taste test.
If you are also interested in our brewery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location: Australia
Website:https://www.dustylizardbrewing.com.au/
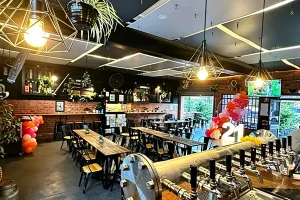
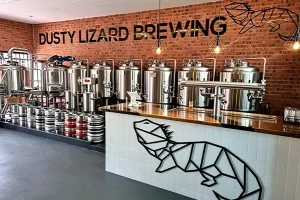
Dusty Lizard Brewing is a craft brewery and brewpub based in Australia, known for producing flavorful, approachable beers for the local market. As demand for their beers continued to grow, the brewery sought a compact yet professional brewing system that could deliver consistent quality, efficient operation, and room for future expansion.
In 2020,After evaluating several equipment suppliers, Dusty Lizard Brewing selected Meto as its brewing equipment partner, based on system reliability,
hygienic design, and technical support experience.
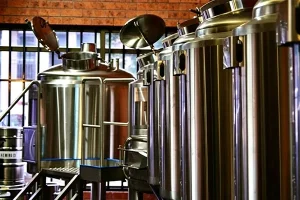
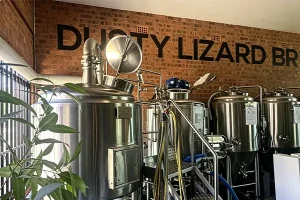
Meto supplied a complete 400 L brewing and fermentation solution, designed to support stable production and flexible beer styles.
With the installation of the 400 L Meto brewing system, Dusty Lizard Brewing successfully achieved:
•Increased production capacity while maintaining a compact footprint
Improved process consistency through precise digital control
•Enhanced beer quality and stability via professional fermentation and bright tank design
•Higher operational efficiency with streamlined cleaning and temperature management
If you are also interested in our brewery equipment, please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.
Location:Guayaquil,Ecuador
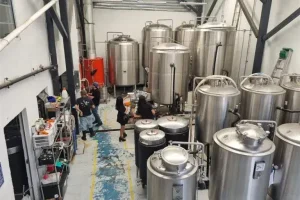
In 2016, we established a partnership with Django Cerveza Artesanal, a renowned craft beer brand in Ecuador, to provide tailor-made brewing solutions for its craft beer bars. We designed and delivered a complete 300L industrial-grade beer production system, including key processes such as mashing and fermentation, ensuring the consistent production of high-quality beer.
The following are the main configurations for purchasing brewery equipment:
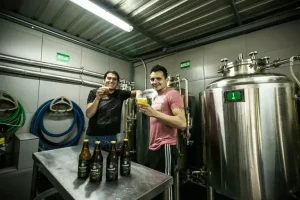
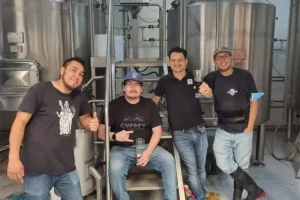
The name “Django” embodies “awakening” – a celebration of Ecuador’s burgeoning brewing culture, and an invitation to rouse your senses.
Complementing the exceptional brews is one-of-a-kind steampunk ambiance, where industrial charm meets cozy warmth. Pair your beer with thoughtfully curated, delicious dishes, designed to elevate every flavor and create a truly unforgettable experience.
If you are also interested in our brewery equipment , please feel free to contact us Meto Equipment. We will recommend the most suitable brewery equipment depending on your requirements and provide you with the most comprehensive and high-quality services.